
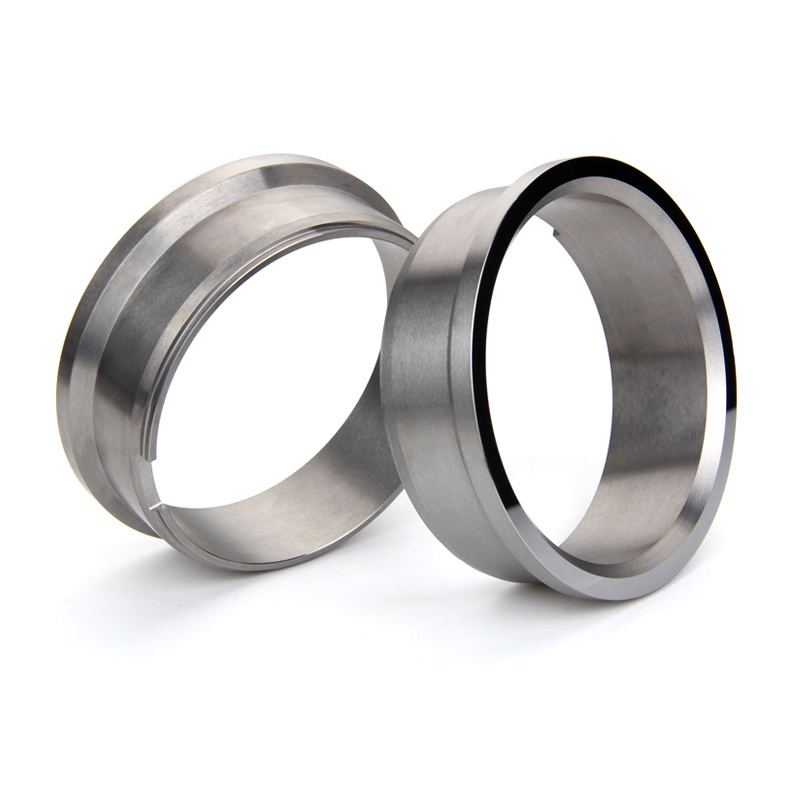
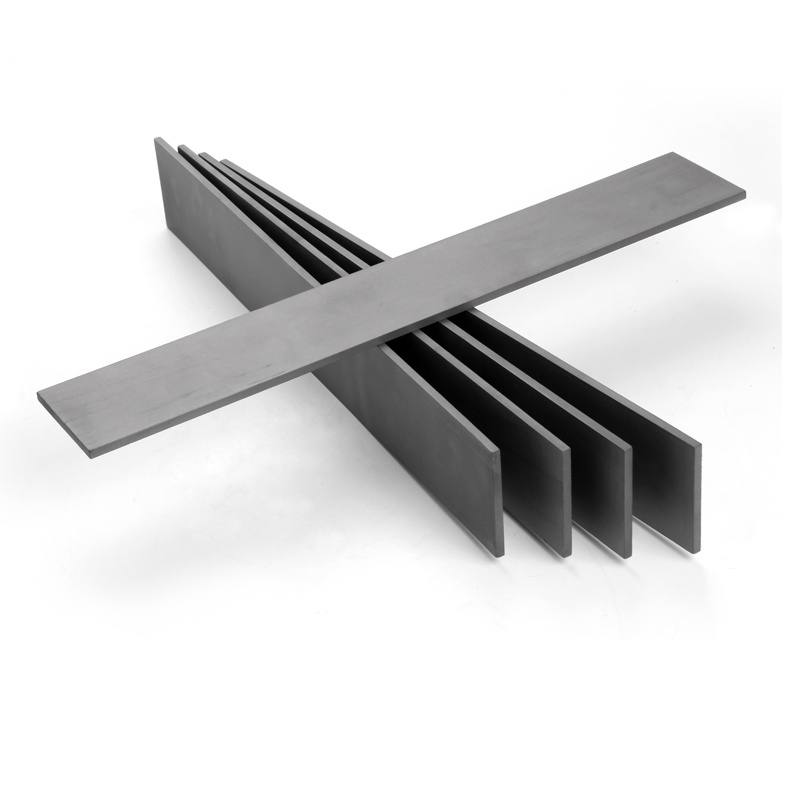
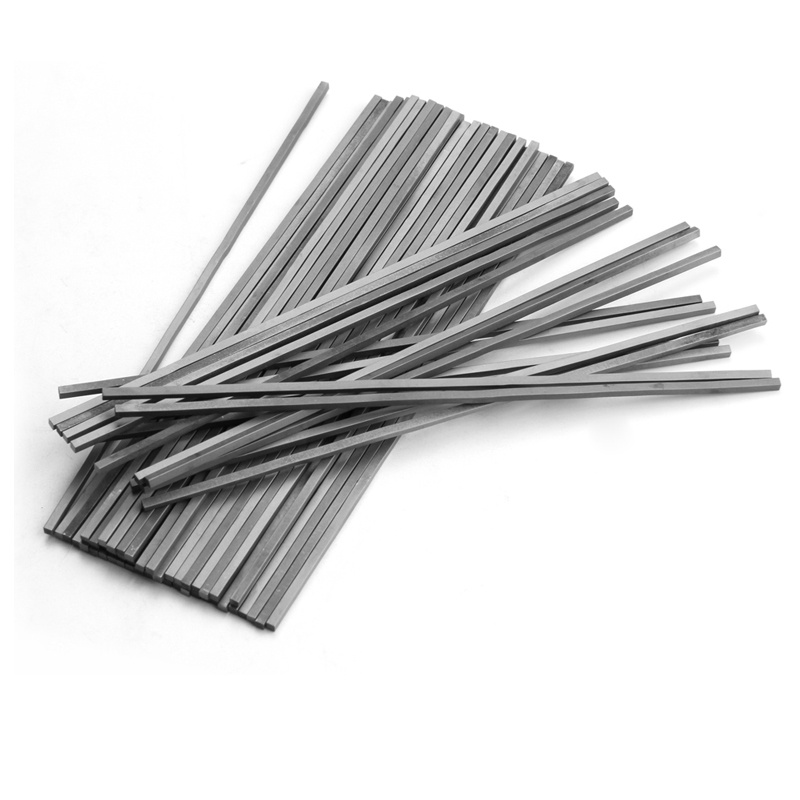
tungsten carbide composite brazed bar
Key words:
hard metal
Classification:
Brazed bars
- 产品描述
-
- Commodity name: tungsten carbide composite brazed bar
- Commodity ID: 1310963843060092928
ProductdetailsTungstenleadfishingsinkermoldsThefishingsinker/weightismadebyraremetal-Tungsten,itisanidealsubstituteoftheleadfishingsinker.It'sstrongadhesive,semi-solidstate,softforalongterm.TungstenHeavyAlloysconcentratemaximumweightinthesmallestpossiblespace.Theyaremoreoftentobeusedascounterweightinsportingfield,suchasfishingsinkers,golfweights,etc. ProductNameWholesaleTungstenFishingWormWeight,SinkerMaterial97%PureEcoFriendlyTungstenColorBlack,darkgreen,darkbrown,ect..BrandJinboshiSize1/161/83/161/45/163/81/25/83/41oz,1.8g3.5g5.3g7g8.8g10.5g14g17.5g21g28g,3/327/161-1/41-1/21-3/42FetruesEchoFriendly,highdenistyShapeBullet,wormweight,flippingweightUsedfishingtackle,fishingsinker&fishingweight
Tungsten carbide composite brazed bar

tungsten carbide composite brazing bar it is made of by sintering tungsten carbide scrap and elastic matrix alloy,Outer layer of the special flux and coloring is marking scrap grade,the composition of sintering tungsten carbide scrap is mainly CO and WC,The hardness is HRA 89~91,tire body matal is Ni and copper alloy,strength can up to 690MPa, hardness HB≥160.
tungsten carbide composite brazing bar usage:
it is mainly used for surfacing welding the oil, mining, coal mining, geology, construction and other industries in some serious wear and tear or artifacts of both cutting.Such as: milling shoes, grinding, centralizer, reamer, drill pipe joints, hydraulic cutter, scraper, plough planer knives, core bit, piling drill, twist drill, etc.
there are eight grades according the size of tungsten carbide scrap
grade
size (mm)
scrap size (mm)
color
YD-9.5
9.5
9.5~6.5
dark green
YD-8
8.0
8.0~6.5
dark blue
YD-6.5
6.5
6.5~5.0
red
YD-5
5.0
5.0~3.0
yellow
YD-3
3.0
3.0~2.0
pink
YD-10mesh
10mesh
10~18mesh
light green
YD-18mesh
18mesh
18~30mesh
light green
YD-30mesh
30mesh
30~50mesh
light yellow
The oxyacetylene butt, the operating process is as follows:
(1) clean up the workpiece, make the welding workpieces surface with metallic luster.
(2) the flat position of welding, therefore can use the appropriate clamping fixture for control of surfacing layer thickness, thick piece of available.
(3) with a neutral flame preheating, flame core not contact surface, the distance to 25 mm is advisable.
(4) carbide surfacing welding layer.With YD type electrode surfacing, the use of neutral flame (can be slightly carbonizing flame) tip is steady on the workpiece surface movement, the flame of the alloy electrode heating (be careful not to make flame cone tip contact alloy particles), tire body in the electrode alloy melt, carbide particles are also falling.Before the tire body of molten metal solidification, the particles arrange, can use left hand of the alloy electrode fingers, or another person holding a base electrode or pull rod on graphite rod in a quick stir particles, making them evenly aligned neatly.Surfacing layer thickness control according to the requirements of design.
(5) after the workpiece welding, where no ventilation, slow cooling, cannot quench, conditional usable asbestos blanket cover.
(6) the workpiece after cooling to room temperature, if necessary, grinding surface surfacing to required size and shape.
(7) clean up the workpiece, remove all splash, slag, etc.
Previous Page
Product inquiry
Note: Please leave your contact information and our professionals will contact you as soon as possible!
Contact Person: Teresa
Address: Building 2, Dahan Hewlett-Packard Industrial Park, Tianyuan District, Zhuzhou City, Hunan Province China
Concerned about the public.